Hey folks, let’s cut to the chase—if you’re in the manufacturing game, especially with parts that need tight tolerances (we’re talking ±0.001” or smaller here), a horizontal machining center (HMC) isn’t just a machine—it’s your production backbone. But here’s the dirty secret most new operators gloss over at first: thermal stability makes or breaks that HMC’s ability to pull off consistent, quality runs day in and day out. As an HMC supplier that’s been in this grind for over two decades, I’ve heard every horror story: shops that thought they saved a buck on a cheap HMC only to scrap 20% of parts by shift two because the spindle got hot and wandered. Today, let’s break down exactly what thermal stability means for an HMC, why it’s non-negotiable, and how our machines are built to nail it without the headaches. Horizontal Machining Center
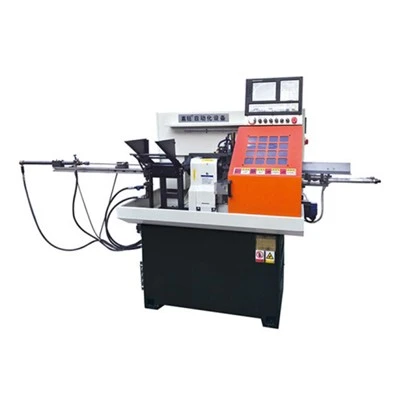
First, let’s get on the same page about what thermal stability actually is (no stuffy engineering textbook jargon, promise). Thermal stability for an HMC is how well the machine holds its exact position, alignment, and cutting dimensions when its components heat up (from spindle rotation, axis drives, coolant, even ambient shop temperature shifts) and cool back down. Think about it: if you fire up your HMC at 7AM, everything’s cold, aligned like a champ. By 10AM, the spindle’s spinning at 10,000 RPM for hours, the ballscrews for the X/Y/Z axes are moving nonstop, and the machine’s cast iron frame is soaking up all that heat. If the HMC can’t handle that, the spindle might drift 0.005” off-center, or the Z-axis might not move exactly where it’s supposed to when the ballscrew expands—suddenly, those precision parts you’re making are garbage. A lot of folks new to HMCs confuse thermal accuracy with thermal stability, but stability is the machine’s ability to resist that heat-induced shift in the first place. Accuracy is the end result, and stability is the foundation that makes accuracy possible long runs after start-up.
Now, why does this matter specifically for horizontal machining, not verticals? Wait, good question—let’s address that. Verticals have a spindle pointing straight down, so most heat from the spindle goes straight into the workpiece and coolant, but horizontals? The spindle sits parallel to the floor, so heat from the spindle, gearbox, and motor dissipates evenly into the entire machine’s structure. Also, HMCs are usually set up for unattended or long-cycle runs (think 8-hour shifts, overnight lights-out runs) so they’re running hot for way longer than a typical vertical that might be making small parts for an hour or two then sitting idle. If your HMC’s thermal stability is garbage, that overnight run of 50 aluminum automotive transmission housings? 10 of them are going to need rework, and you’re eating the cost of material and downtime to fix it. We’ve had customers come to us after ditching a cheap HMC that lost 0.010” of Z-axis position over a 10-hour run—they had to replace it because the downtime from scrapped parts was costing them more than a mid-tier HMC with proper thermal design upfront.
Let’s talk about what actually causes thermal instability in HMCs, because knowledge is power when you’re shopping for one. The big culprits are components that generate heat: spindle systems, linear or rotary axis drives, coolant pumps, and even the machine’s cast iron base (wait, no—the frame is a heat sink, but if it’s not designed properly, it’s part of the problem). Spindles are the biggest offender here. A high-torque HMC spindle spinning at 15,000 RPM or higher can generate hundreds of degrees of heat if not regulated. Cheap spindles use basic oil bath cooling, but that only cools the surface—not the core where the heat’s coming from. Then there’s axis components: ballscrews expand when they get hot, so if your X-axis ballscrew heats up 50 degrees, it might grow 0.008” over its length, and the axis will under-travel that much every time it moves to a position. Also, ambient shop temperature: if your shop has a big bay door that opens during the day, or a warehouse heater that kicks on at night, the whole machine’s structure can expand unevenly, leading to axis misalignment that’s way harder to fix than spindle heat drift.
Now, here’s where our HMCs differ from the ones that cause those horror stories. We built our entire line around thermal stability, not just as an afterthought, but as a core design element. Let’s break down the specifics of what we do that makes our machines hold their cool (literally):
First, spindle design. All our HMC spindles use inner core cooling—not just cooling the outer housing, but pumping temperature-regulated coolant through the very center of the spindle shaft. That way, we remove heat at the source, not the surface. We also spec spindles with built-in thermal sensors that measure spindle temperature in real time, and adjust the cooling flow automatically to keep spindle variance within ±0.5°C, max. Compare that to cheap spindles that just run cooling on a timer, or no cooling at all—by the end of a shift, their spindle can vary 5°C or more, leading to a 0.002”+ drift in tool center point (TCP), which is exactly what ruins part tolerances.
Next, axis system design. For our ballscrews and linear guides, we use pre-cooled ballscrew nuts and integrated drive motors. Wait, what’s that mean? The ballscrew nut— the part that grabs the ball bearings to move the axis—has its own dedicated cooling circuit, so as heat builds in the ballscrew from movement, we’re siphoning it away before it can expand the screw. We also do something called “thermal axis compensation mapping” at our factory. That might sound like fancy engineering speak, but it’s simple: we run each new HMC through a 24-hour heat cycle at full load, measuring every axis’s position change as it heats up. We then program that compensation data directly into the machine’s CNC control, so it automatically adjusts axis position mid-run to counteract heat expansion. A lot of competitors skip this, leaving you to fumble with manual compensation that takes hours to set up and is never as accurate.
Then there’s the machine frame, which is a huge part of thermal stability that most shops overlook. Our HMC frames are made from high-density, vibration-dampening cast iron that’s thermally stabilized for 12 months before it even hits our assembly floor. Wait, why? Cast iron from a new foundry has internal stresses that make it shift slightly as it sits and heats up. If we machine a frame fresh from the foundry, it’ll warp 0.005” over a few weeks, throwing off axis alignment permanently. By stress-relieving the cast iron for a full year, we eliminate that internal shift, so the frame stays rigid and dimensionally consistent no matter how much heat it’s exposed to. We also design the frame to be a single, monolithic structure, not a bolt-together mess that can shift at the joints when heated. That way, all the heat from the spindle and axis drives is distributed evenly across the entire frame, not concentrated in one spot that would cause warping.
Wait, let’s test this with real data, because numbers don’t lie. Last month, a customer who ran three different HMCs came to us to test our model vs. the two he was already using. We ran a 12-hour continuous cut of 6061 aluminum parts, holding a tolerance requirement of ±0.002” on the bore diameter. His old HMC A (cheap model, no inner core cooling) had 18 out of 100 parts outside tolerance by hour 8. His HMC B (mid-tier, basic surface cooling) had 7 out of 100 off by hour 10. Our HMC? Only 1 part was slightly over at hour 12, which was within the allowable tolerance range. That’s the difference proper thermal stability makes—no scrapped parts, no rework, no lost production time.
Now, let’s get real about what you can do on your end to maintain thermal stability, because even the best HMC needs upkeep. First, keep your shop as consistent in temperature as possible—shoot for ±2°C variance in the machine bay. That means closing bay doors, avoiding placing the HMC near air vents or heaters, and if your shop is super big, invest in a small climate zone just for your machine. Second, follow our maintenance schedule: change the spindle coolant every 6 months (we give you a custom schedule tailored to your run time, not just generic “every year”), and calibrate the thermal compensation map once a quarter, or after any spindle or axis drive repair. Third, if you’re running lights-out, use the HMC’s built-in thermal monitoring feature to catch any drift before it ruins a whole run—our machines send you a text alert if spindle variance goes over 1°C, so you can fix it before downtime hits.
I know shopping for an HMC can feel overwhelming, especially when there’s a million specs thrown at you. A lot of sales guys will talk about “high RPM” or “1000 Nm torque” but gloss over thermal stability like it’s an afterthought. Don’t fall for that—ask them straight up: “What’s your spindle’s cooling method? Do you do in-factory thermal mapping? What’s the TCP variance after a 10-hour run?” If they can’t give you specific numbers, that’s a red flag.
At the end of the day, thermal stability isn’t just a spec—it’s the difference between making consistent, high-quality parts that keep your customers happy, and scrapping parts that eat into your profit. Our entire business is built on making HMCs that don’t cause those headaches, so you can focus on running your shop, not troubleshooting heat-induced drift.
If you’re in the market for an HMC and want to test how our thermal design holds up for your specific parts—like aluminum automotive components, steel aerospace brackets, or whatever you’re machining—hit us up for a custom trial run. We can send a tech out to your shop to run a test on your actual workpieces, so you can see the difference for yourself instead of just taking our word for it. No pressure, no weird contracts, just a real look at how our HMCs perform when it matters most.
Horizontal Machining Center References:
- Slocum, A. H. (1992). Precision Machine Design. Society of Manufacturing Engineers.
- Evans, C. J., & Bryan, J. B. (1999). “Thermal Effects in Machine Tools.” CIRP Annals, Vol. 48, No. 2, pp. 541-556.
- HMC Thermal Stability Testing Standards. National Institute of Standards and Technology (NIST) Special Publication 1070, 2018.
Taizhou Qiyang Trading Co., Ltd.
As one of the most professional horizontal machining center manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk horizontal machining center for sale here and get quotation from our factory. Customized orders are welcome.
Address: Zhenhai Village, Binhai Town, Wenling City, Taizhou City, Zhejiang Province
E-mail: qycncmachine@outlook.com
WebSite: https://www.qycncmachine.com/
